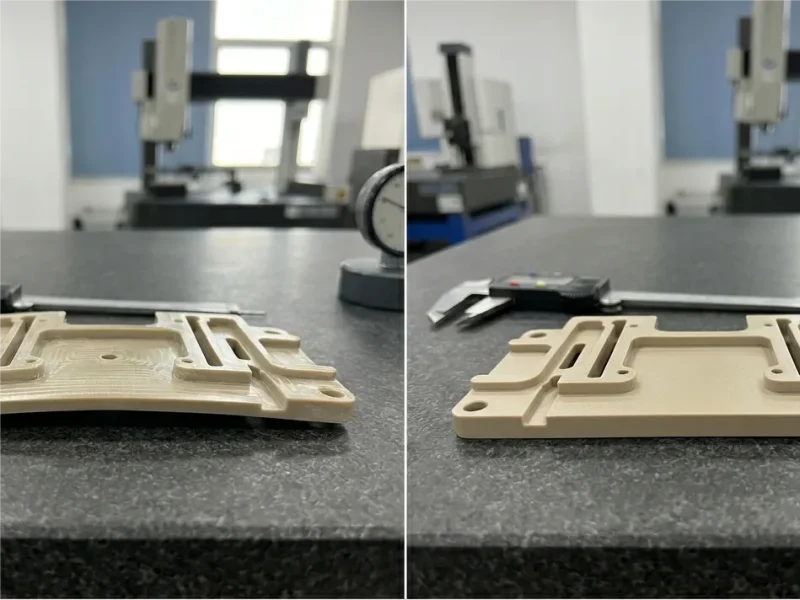
For a source manufacturer of PEEK rods and plates, the core challenge in production lies in managing “Crystallinity Control” and “Internal Stress Relief.”
As a semi-crystalline polymer, PEEK’s dimensional stability is highly sensitive to cooling rates and stress distribution.
Below is a systematic approach to mitigating warpage across three critical stages: Injection Molding, CNC Machining, and Post-Processing.
1. Injection Molding: Precision Thermal Management
Injection molding is often where warpage originates. The objective is to ensure uniform and complete crystallization within the mold.
High-Temperature Mold Control (Critical): Mold temperatures must be maintained between 170°C and 200°C. If the mold is too cold, the PEEK melt quenches into an amorphous state, leading to catastrophic dimensional shifts later. We recommend using oil-based mold temperature controllers with PID closed-loop systems to minimize temperature gradients across the mold surface.
Optimized Cooling Systems: Traditional straight-line cooling channels often lead to uneven thermal distribution. For precision parts, consider 3D-printed conformal cooling channels that follow the part geometry, ensuring synchronized cooling and significantly reducing residual stress.
Gate and Runner Optimization: Utilize larger gates (such as fan gates) to minimize shear heat and flow-induced stress. It is vital to maintain uniform wall thickness wherever possible to prevent asynchronous shrinkage between thick and thin sections.
2. CNC Machining: Symmetrical Cutting and Thermal Regulation
When machining PEEK rods or plates, the removal of material can “unbalance” internal stresses, causing the part to bow or twist.
Symmetrical Machining (Balanced Material Removal): Never remove the full allowance from one side in a single operation. Implement a flip-machining strategy: if 5mm must be removed, mill 2.5mm from the top, flip the workpiece, and mill 2.5mm from the bottom. This balanced approach neutralizes stress release.
The “Roughing-Annealing-Finishing” Cycle: For high-tolerance components, a three-step process is essential. Perform rough machining leaving a 1–2mm buffer, subject the part to an intermediate annealing cycle to release stresses, and then proceed to final precision finishing.
Heat Dissipation: Use sharp, high-positive geometry tools. Opt for high feed rates and moderate spindle speeds to ensure heat is carried away by the chips rather than soaking into the part. Utilize high-pressure air cooling to prevent localized softening.
3. Material Pre-treatment & Post-Processing: Stress Relief via Annealing
Annealing is the most effective method for stabilizing PEEK dimensions for both molded and machined parts.
Raw Material Pre-drying: PEEK is hygroscopic. Even trace moisture can cause bubbling and structural degradation during high-temperature processing. Dehumidify resin at 150°C for at least 3–4 hours to ensure a moisture content below 0.02%.
Finished Product Annealing: Place the finished or semi-finished parts in an industrial oven. Gradually ramp the temperature to 200°C–220°C (above the Glass Transition Temperature $T_g$ but well below the Melting Point $T_m$). Hold for several hours (depending on wall thickness), then slowly cool at a rate of approximately 5°C per hour until it reaches room temperature. This allows molecular chains to relax and optimizes crystallinity.